


Rack Integrated Tote Lift
Lift Structure Integrated Directly into the Racking
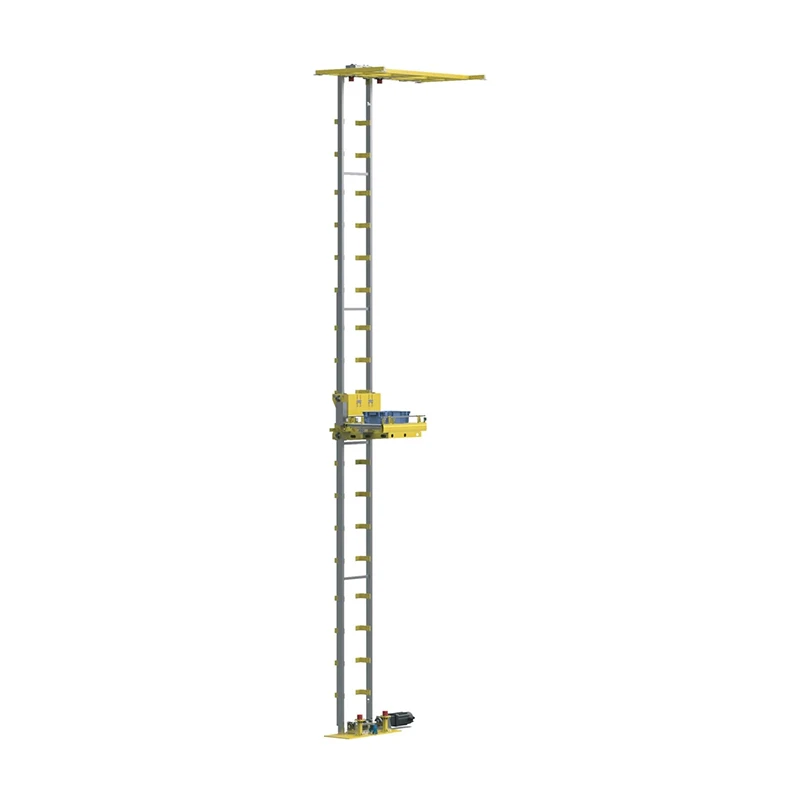
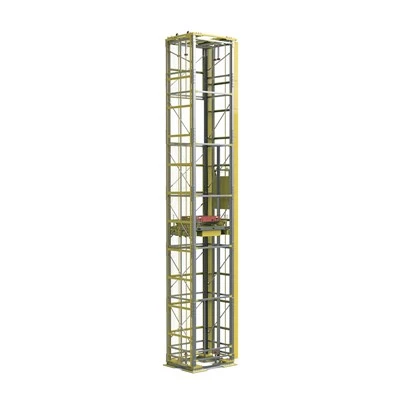
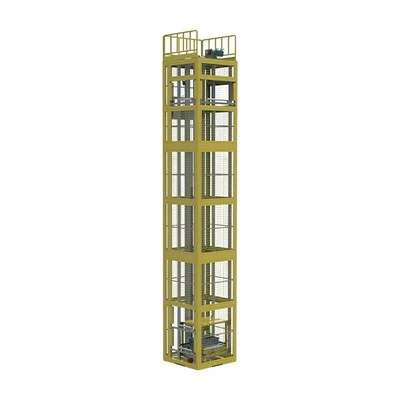
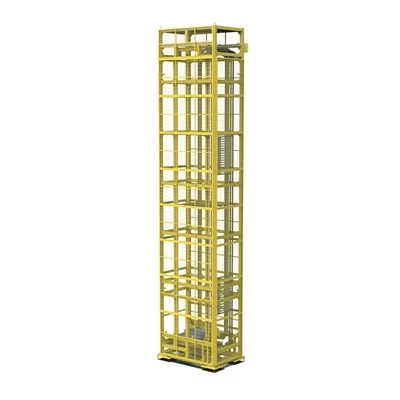
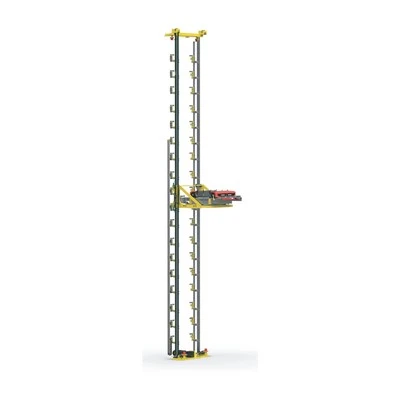
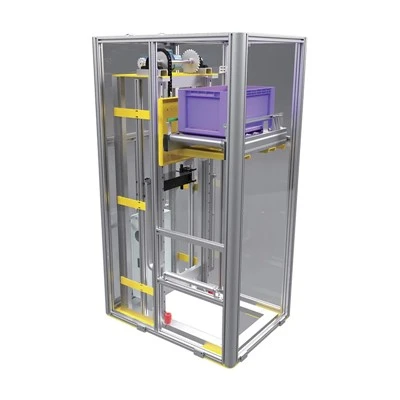
The RLFH-0100 is a vertical tote lifting system designed with its lifting columns integrated directly into the rack structure. Instead of installing a separate standalone lift beside the storage system, the lifting channel becomes part of the racking layout itself.
This structure helps reduce the additional floor area normally required for independent vertical conveying equipment. It is suitable for tote storage systems where warehouse space utilization, compact equipment layout, and future expansion need to be considered together.
The Rack Integrated Tote Lift uses a modular assembly concept. Additional modules can be added as the rack extends upward, allowing the lifting height or access positions to be adjusted according to the warehouse layout. This provides useful flexibility for new automated storage projects as well as systems where additional rack levels may be planned later.
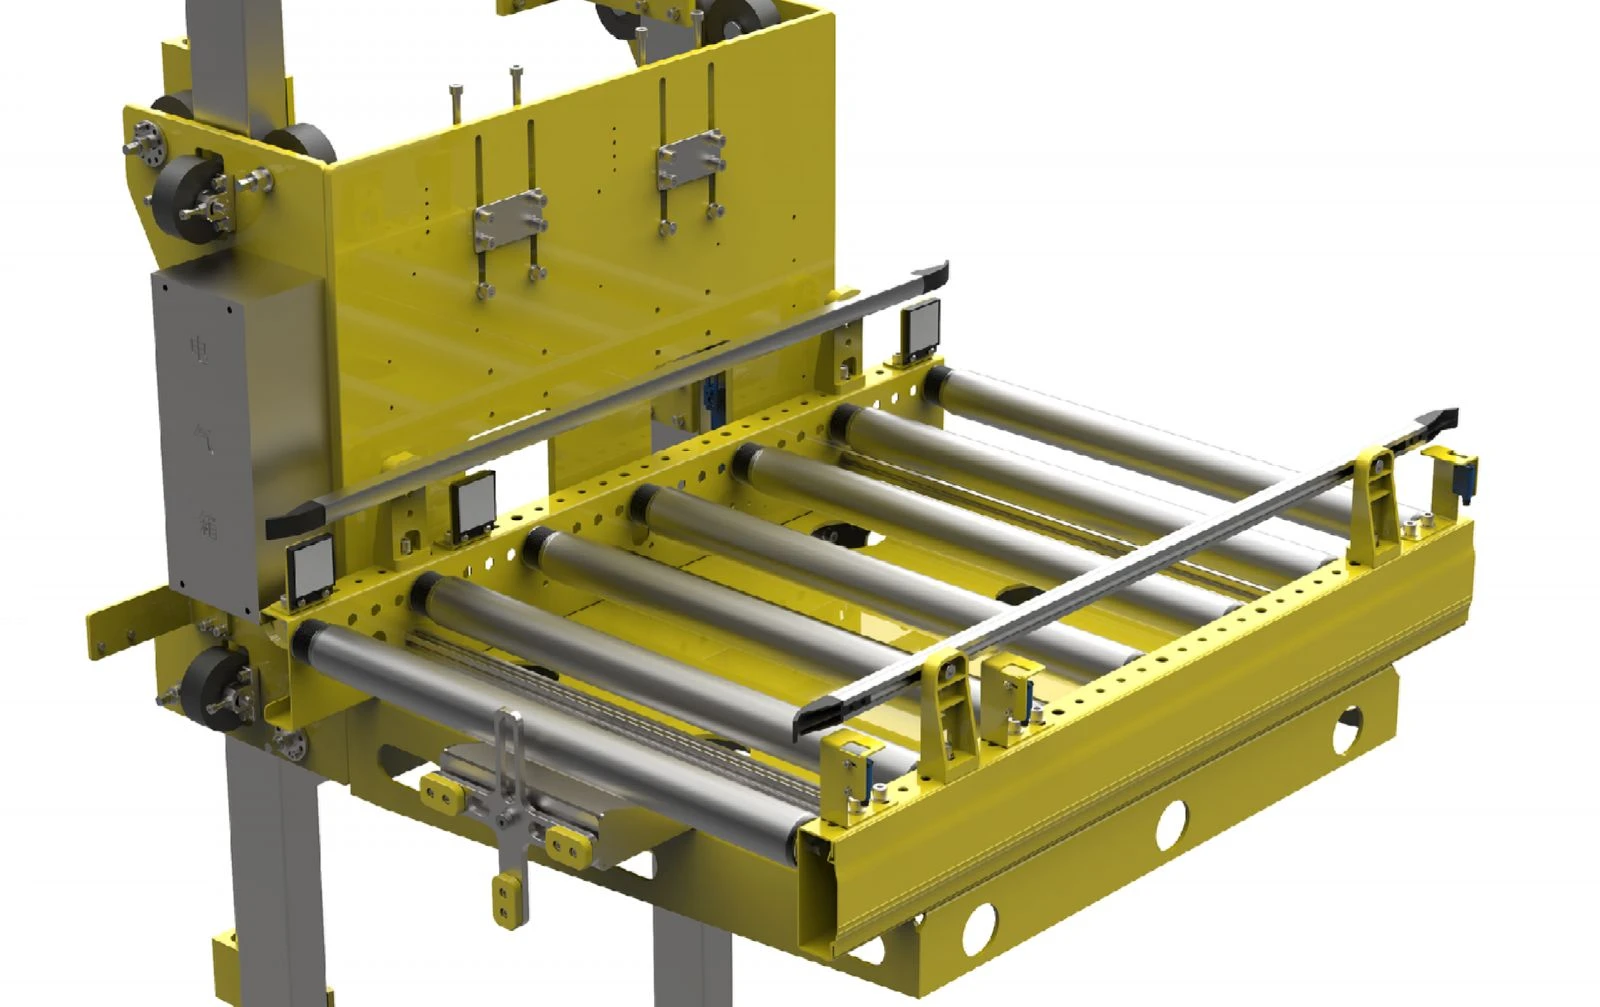
The system supports both single-level and double-level carriage configurations, allowing the lifting unit to be matched to different tote handling arrangements.
High-Speed Vertical Handling up to 24 m
- The RLFH-0100 supports tote sizes of 600 × 400 mm and 800 × 600 mm. Maximum load capacity is 100 kg.
- The minimum conveying height is 450 mm. Maximum equipment height is 24 m, with customization supported within this range.
- Unloaded lifting speed can reach 240 m/min with acceleration of 4 m/s². Under load, maximum lifting speed is 180 m/min with acceleration of 3 m/s².
- The lifting mechanism uses a servo motor with synchronous belt transmission. Lifting motor power is 7.5 kW.
- For automated tote storage systems with frequent movements between different rack levels, these parameters allow the Rack Integrated Tote Lift to support high-frequency vertical transfer without requiring a separate lift tower outside the racking.
Positioning, Conveyor Interface and Project Planning
Positioning can use laser distance measurement or barcode positioning. Positioning accuracy is ±2 mm, helping the carriage align accurately with target rack levels or access points.
The platform uses roller conveying with a maximum speed of 30 m/min. Roller power is 50 W.
The specified operating environment is -10°C to 45°C, relative humidity should not exceed 85%, and operating noise is specified at no more than 75 dB(A).
During project planning, buyers should confirm rack height, tote dimensions, highest storage level, inlet and outlet positions, actual load, and required throughput. If future rack expansion is expected, the modular extension requirements can also be considered during the initial design stage.
Because the lifting structure is integrated into the rack, mechanical interfaces between the rack and lift should be confirmed together rather than designed separately.
Engineering Support for Integrated Storage Systems
in one-stop service
Anhui Rayo Automation develops both intelligent logistics equipment and digital systems. Its technical teams include mechanical design, electrical control, software development, and system integration personnel.
The company holds CMMI Level 3 software capability maturity certification. Manufacturing resources include gantry machining centers, CNC machining centers, laser cutting machines, 3D printers, CNC lathes, and bending machines.
For a Rack Integrated Tote Lift project, support can cover requirement analysis, solution design, manufacturing, installation, commissioning, and subsequent expansion coordination. Rayo also has domestic cross-regional engineering resources and overseas offices that can support customized lifting heights and system interfaces.

Hot Tags: rack integrated tote lift, China rack integrated tote lift manufacturers, suppliers, factory
Previous
Continuous Tote LiftYou Might Also Like
Send Inquiry